Why AFT 11HS
‘V’ Shape, Straight Process Zone, Double Heater, False Twist, Manual Doffing Draw Texturing Machine
- Watch our video
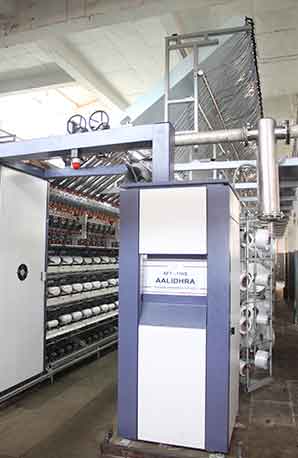
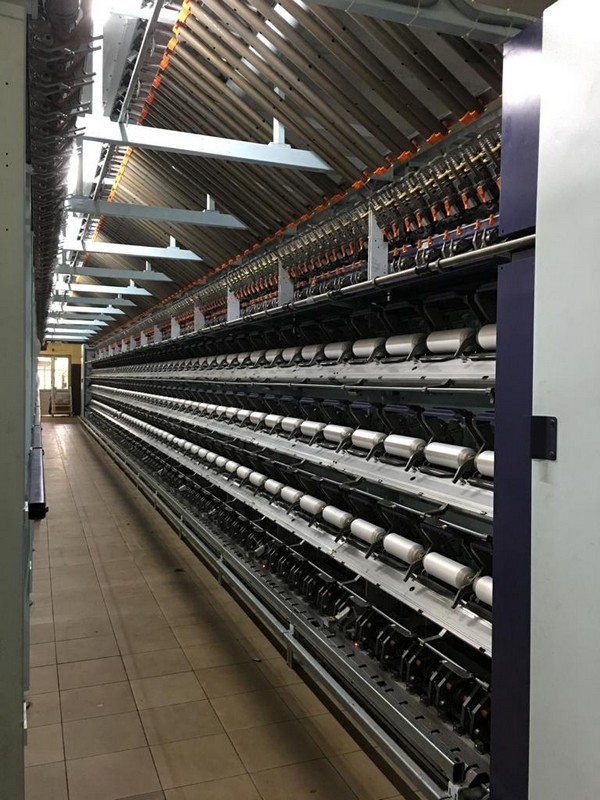
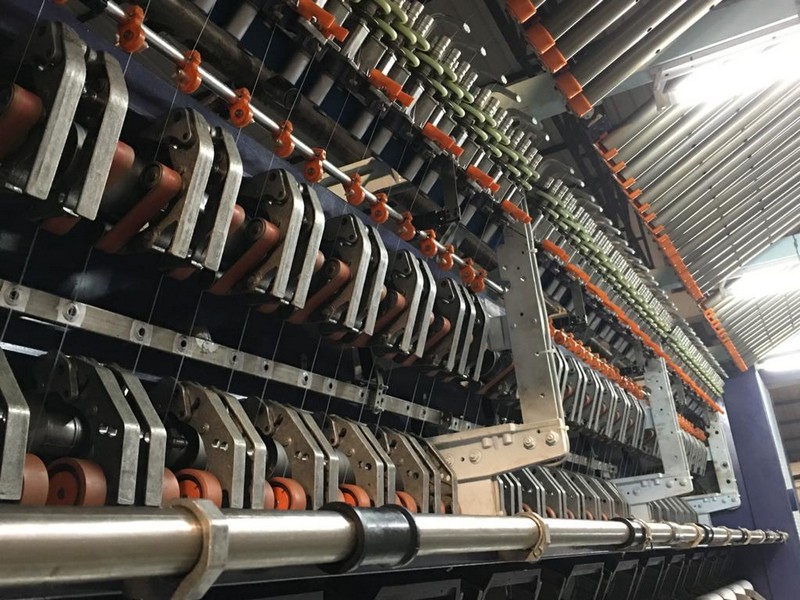
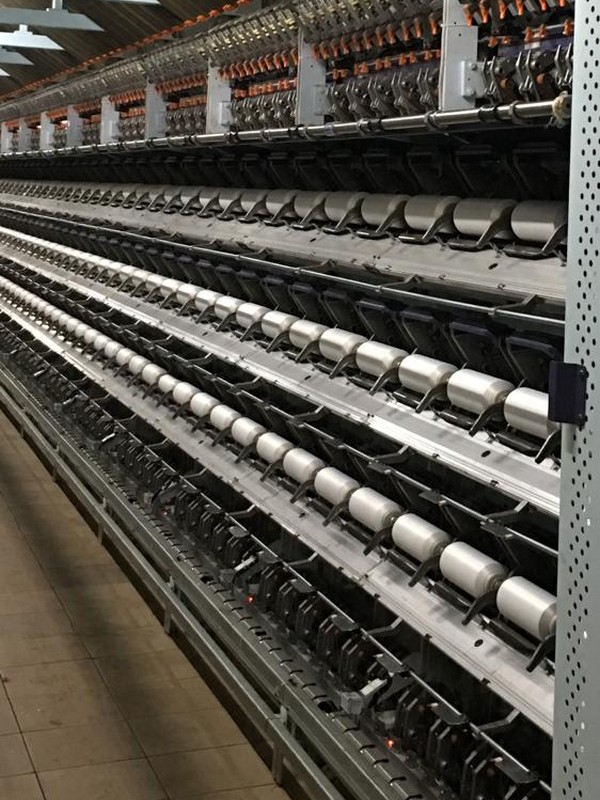
M/C Speed: 1200 Meter/min. Mechanical speed.
Process Denier Range: 30 to 300 denier (33 to 333 dtex) Polyester (PES), polyamide (PA) or polypropylene (PP)
Min./Max. No. Of position: Min. 24 / Max. 360
Power Consumption: 0.55 KW / Kg of production of 75 Denier DTY @ 900 Meter/Min. process speed, which depends on machine maintenance, end product quality requirement and ambient condition, 28 ~ 32 degree Celsius.
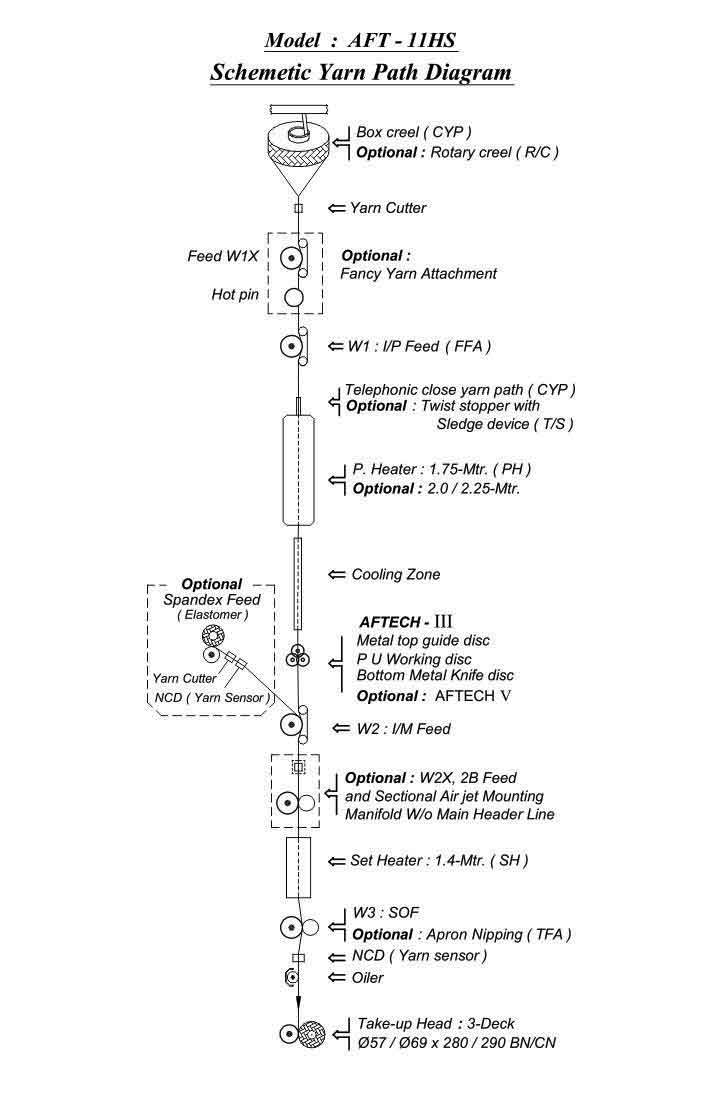
Feed Creel: Box type, close yarn path, 1+1 Rotating package holder per position to accommodate Max. package Dia. 440 mm.
Yarn Feed Shafts:
– W1 & W2 Feed shaft with Apron Nipping
– W3 feed Shafts with Nip Roller Nipping
Texturing Heater:
– 1.75 Meter Long, Close Contact type, Vapour phase group heater with fix guide telephonic yarn path
– Temperature range: 160°C to 240°C
Setting Heater:
– 1.4 Meter Long, Non-Contact type, vapour phase group heater
– Temperature range: 140°C to 240°C
Cooling Zone: 1250 mm. long, tubular type, peripheral tangential yarn path
Friction Twist head:
– AFTECH III, Tangential belt drive, “S” twist or “Z” twist or Alternate twist with 1-4-1-disc configuration, suitable up to 1-6-1 disc Combination
– 9mm X 54.5 Diameter PU working disc
– Top metal Guide disc
– Bottom metal Knife-edge disc
Tack – Up Head:
– Manual doffing
– Heavy Duty Cradle with finger protection guard on cam box.
– 6/12/18 degree Bi-conical package build up
– 57 OR 69 mm Diameter, 280/290 mm paper tube length
– Max package Diameter: 240mm.
– Max Package Wt.: 6.5 Kg. @80~100 finish denier
– Traverse speed: Up to 600 CPM
– Multi stroke, axial winding program
Oiling Device: 64 mm. Diameter grooved oil Roller
Control Panel: High security Panel with isolated invertor drive heat sink zone with collective cutter system or battery back up to protect PU disc in case of power failure.
Add on / alternate optional supply for enhancing specific DTY product quality and productivity.
Rotary Creel (R/C): Rotary creel, 1+1 Rotating package holder per position facilitates loading of creel from either side of the creel in place of Box Creel as a Std. scope of supply
Twist Stopper (T/S): Twist arrester wheel at entry of the texturing heater with manual string up sledge mechanism in Place of fix guided telephonic yarn path as a Std. scope of supply for better process control/stability.
Texturing Heaters (PH): 2.0/2.25 Meter long heater to optimize processing of courser denier range with better process control in place of 1.75 meter heater as a Std. Scope of supply.
Split Control: Independent process parameter setting/control of both side of the machine
Spandex (Elastomer) Feeder: Spandex drafting/feeding with shortest possible and straight yarn path
2B (W2X) Feed shaft: Additional 4th feed shaft with Nip Roller above set heater for better intermingling control (Apron Nipping at an additional cost)
Apron Nipping: Apron nipping at 2B (W2X) feed in place of Nip roller as a Std. scope of supply.
Plying Facility: Doubling roller guide attachment to process 2 Ply yarn with or w/o additional NCD above W1 (I/P) feed to avoid faulty yarn processing
Hard/Soft Package Formation: Take Up Cradle with pressure adjustment through dead weight to produce regular and soft package for textured yarn dying application
Doff Timer: Doff timer for random, sectional or side/machine wise equal length doffing indications and production efficiency monitoring system
OLT monitoring System: On line tension monitoring (OLT) from Fiber Vision, UK, with production efficiency monitoring system and equal length package indication/control facility (PC and required Window OS are in Buyer’s scope of supply)
False twist unit Disc:
a) Ceramic leading disc (CLD) against Metal one, Top Guide Disc.
b) Ceramic knife-edge disc (CKED) against Metal one, Bottom Disc.
c) Ceramic Working disc (CWD) against PU disc.
AFTECH V: Friction twist unit with larger Dia. 60 mm X 12 mm Thick PU disc with suitable Top and Bottom guide disc, 1-4-1 or 1-5-1 disc configuration against AFTECH III
FOF: Four operating facility for quick loading the machine providing additional Air suction line, trolley and Threading Gun
Main Header line: Compressed Air header line though the machine length with connecting accessories to the sectional manifold without air control and pressure regulating valve
Fancy Yarn attachment: A combination of hot pin and additional feed shaft W1X before first feed shaft W1 to produce thick and thin look textured yarn
Machine Lay Out : 3 Deck Take Up, Double sided machine
Machine Length and Width :
| No. Of Position | 240 | 288 | 312 | 336 | 360 |
| Machine Length with | 16.50 mtr. | 19.30 mtr. | 20.70 mtr. | 22.10 mtr. | 23.50 mtr. |
| Door closed | 54’-2” | 63’-4” | 67’-11” | 72’-6” | 77’-2” |
| Machine Width with | ——————–5.750 Mtr. / 19’-00”——————– | ||||
| Box Creel | |||||
| Machine Width with | ——————–6.560 Mtr. / 21’-6” ——————– | ||||
| Rotary Creel | |||||
| Machine Width with 2B (W2X) Shaft & Box Creel | ——————–6.10 Mtr. / 20’ ——————– | ||||
| Machine Width with 2B (W2X) Shaft & Rotary Creel | ——————–6.850 Mtr. / 22’-6” ——————– | ||||
Machine Height:
o With 1.75 Mtr. Heater: 4.16 Mtr. (13’-8”), with 2B (W2X) Shaft: 4.38 Mtr. (14’-5”)
o With 2.0 Mtr. Heater: 4.27 Mtr. (14’-1”), with 2B (W2X) shaft: 4.49 Mtr. (14’-9”)
o With 2.25 Mtr. Heater: 4.41Mtr. (14’-6”), with 2B (W2X) shaft: 4.63 Mtr. (15’-3”)
No. Of position: 192 216 240 264 288 312 336 360
Drive Motor (KW): 46 54 60 66 72 78 84 87
All Heater (KW): 36 40.5 45 49.5 54 58.5 63 67.5
Other Auxiliary (KW): 10 10 10 11 11 11 11 13
Total Power, KW: 92 104.5 115 126.5 137 147.5 158 167.5